What Buyers Should Actually Check Before Placing a First Order
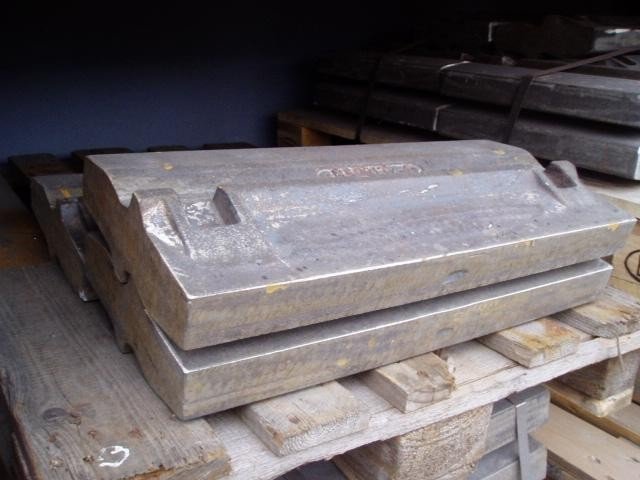
Wear parts buyers are re-examining where their blow bars and shredder hammers come from. Industry forecasts through 2025 describe tariff pressure pushing crusher wear part supply chains to diversify sourcing and localise production, away from regions exposed to trade measures. For many distributors and plant operators, that has meant looking seriously at India for the first time.
This guide is written for that buyer. It is not an argument that Indian foundries are automatically better. It is a practical checklist for judging any wear parts foundry, wherever it sits, because the country of origin tells you far less than the questions below.
Country Is the Weakest Signal You Have
Every casting region has excellent foundries and poor ones. Choosing on country alone replaces one lazy assumption with another. What actually predicts whether a wear part performs is narrower and more boring: the metallurgy is controlled, the heat treatment is consistent, and the same process runs on order fifty as ran on order one.
A supplier who cannot show you how they control those three things is a risk regardless of where their furnace stands. A supplier who can is worth evaluating even if their address is unfamiliar.
The Questions That Separate Suppliers
Do you cast this yourself, or buy it in?
A surprising share of wear parts exporters are trading houses. They take your order, place it with a foundry, and resell. That is not automatically bad, but it means nobody in the chain owns the metallurgy. When a batch underperforms, the trader cannot tell you why, because they were not there when it was poured.
Ask directly whether the parts are cast in the supplier's own facility. Ask how many facilities, and what the casting weight range is. A foundry that casts from a few kilograms to two tonnes has different capability from one that only handles small parts.
What grades do you run in-house?
Wear parts are not one material problem. High manganese steel, high chrome white iron, Ni-hard and alloy steels all behave differently, and the right choice depends on whether your failure mode is abrasion, impact, or a mix.
A supplier who only runs one grade family will recommend that grade for everything, because it is what they have. A supplier running the full range can tell you when their own default is the wrong answer — which is a far more useful conversation.
What documentation comes with each batch?
At minimum you want hardness test reports and material certificates issued per production batch, not per contract. Batch-level records are what let you prove consistency to your own customers, and what lets you investigate properly if one shipment behaves differently from the last.
If a supplier offers a single certificate covering an entire year of orders, that is not batch traceability.
Can you work from a sample or a drawing?
Much of the aftermarket exists because machines outlive their OEM parts support. If you handle older crushers or rebuilt rotors, you will eventually need a part that has no current drawing. Ask whether the foundry develops patterns from worn samples, what that costs, and how long it takes.
This capability is the difference between a supplier who can serve your whole customer base and one who can only serve the newest machines in it.
How to Run a Trial Order Properly
Almost every serious supply relationship starts with a trial. Most trials are run badly, and produce a result nobody can interpret.
Change one thing at a time
If you switch supplier, grade and hammer design in the same trial, and wear life improves, you have learned nothing about which change caused it. Hold the design and the grade constant, and change only the supplier.
Record the baseline before you start
You need the current wear life, the feed being processed, the rotor speed and the reason parts are being changed out — abrasion, fracture, or eye wear. Without a baseline, the trial result is an anecdote.
Run the trial on a representative line
Trials on the cleanest feed or the newest machine flatter every supplier. Run on a line that reflects normal conditions, or the result will not survive contact with the rest of the fleet.
Measure by tonnes processed, not by weeks
Calendar life depends on how much the plant ran. Tonnes through the machine is the only comparison that holds across different periods and different plants.
Costs That Do Not Appear on the Quotation
Buyers comparing suppliers on unit price alone routinely pick the more expensive option without realising it. The costs that decide the real number are:
- Downtime for change-outs — a part lasting 20% longer removes change-outs from the year, and each one costs production hours
- Throughput decay — as hammer or bar weight falls, crushing energy falls with it, and product size and output drift before the part is formally worn out
- Failure risk — one fractured part in a rotor can damage far more than the part itself
- Freight and duty — the landed cost, not the ex-works price, is the number that matters
- Inventory carrying cost — longer lead times mean more stock sitting on your shelf
A part costing more per piece and delivering meaningfully longer service life is usually the cheaper decision. Work in cost per tonne processed rather than cost per piece.
Practical Points for Importing
Agree the price basis explicitly
FOB and CIF quotations are not comparable. Establish which port, which basis, and what is included before you compare two suppliers, or you will compare two different things.
Ask about packaging before the first shipment
Wear parts are heavy and awkward. How they are crated determines whether they arrive intact and how easily your warehouse can handle them. Agree marking and packing specification up front.
Understand the lead time components
Quoted lead time usually covers production. Pattern development, if a new pattern is needed, sits before that. Sea freight sits after. Ask for all three separately so your stock planning reflects reality.
Where India Fits
India has a long-established foundry sector serving domestic mining, cement and steel industries, with export practice built over decades. For a buyer diversifying supply, it offers an alternative country of origin without stepping outside established manufacturing capability.
That is a genuine advantage in the current sourcing environment, but it is not a guarantee of quality — it is a reason to evaluate, not a reason to skip evaluation. Apply the same questions above to an Indian foundry that you would apply anywhere else. A supplier confident in their process will answer all of them without hesitation.
A Short Checklist
- Do they cast in their own facility, and what is the weight range?
- Which grades run in-house, and will they tell you when their default grade is wrong for you?
- Are hardness reports and material certificates issued per batch?
- Can they develop a pattern from a worn sample, and at what cost and lead time?
- Do they ask about your feed and failure mode before recommending a grade?
- Is the price basis, port, packaging and lead time breakdown clearly stated?
The last one matters more than it looks. A supplier who asks what you are crushing before quoting a grade is engaging with your problem. One who quotes immediately without asking is selling you what they have in stock.
About Melco Precisions Pvt Ltd
Melco Precisions Pvt Ltd is an Indian foundry with 40+ years in wear-resistant castings, producing shredder hammers, blow bars and crusher wear parts in high manganese steel, high chrome white iron, Ni-hard and alloy steels. Castings run from approximately 1 kg to 2000 kg per piece across two integrated facilities, with hardness test reports and material certificates supplied per production batch, and manufacturing to OEM dimensions or to customer drawings and samples.
Distributors and importers evaluating supply can find order and shipping information on our distributors page, or review the shredder hammer and blow bar ranges directly.